Soligorsk, st. Zavodskaya, 4
Soligorsk, st. Zavodskaya, 4
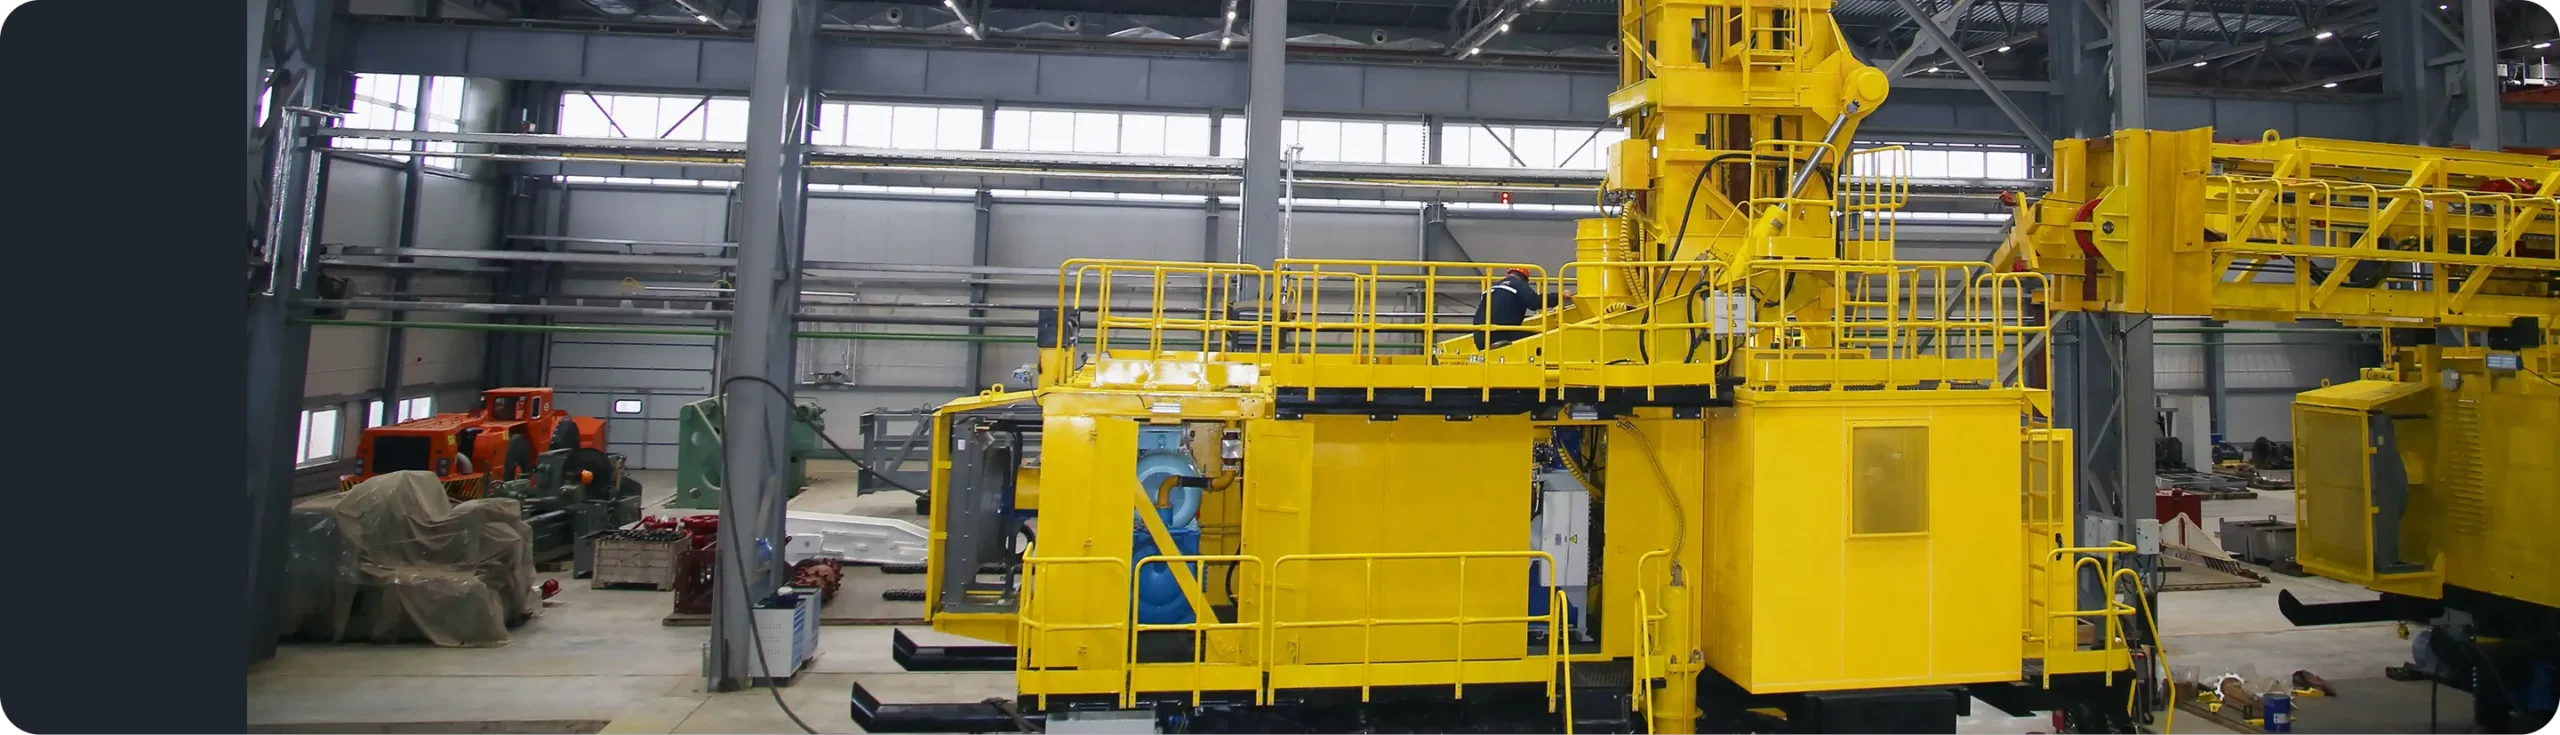
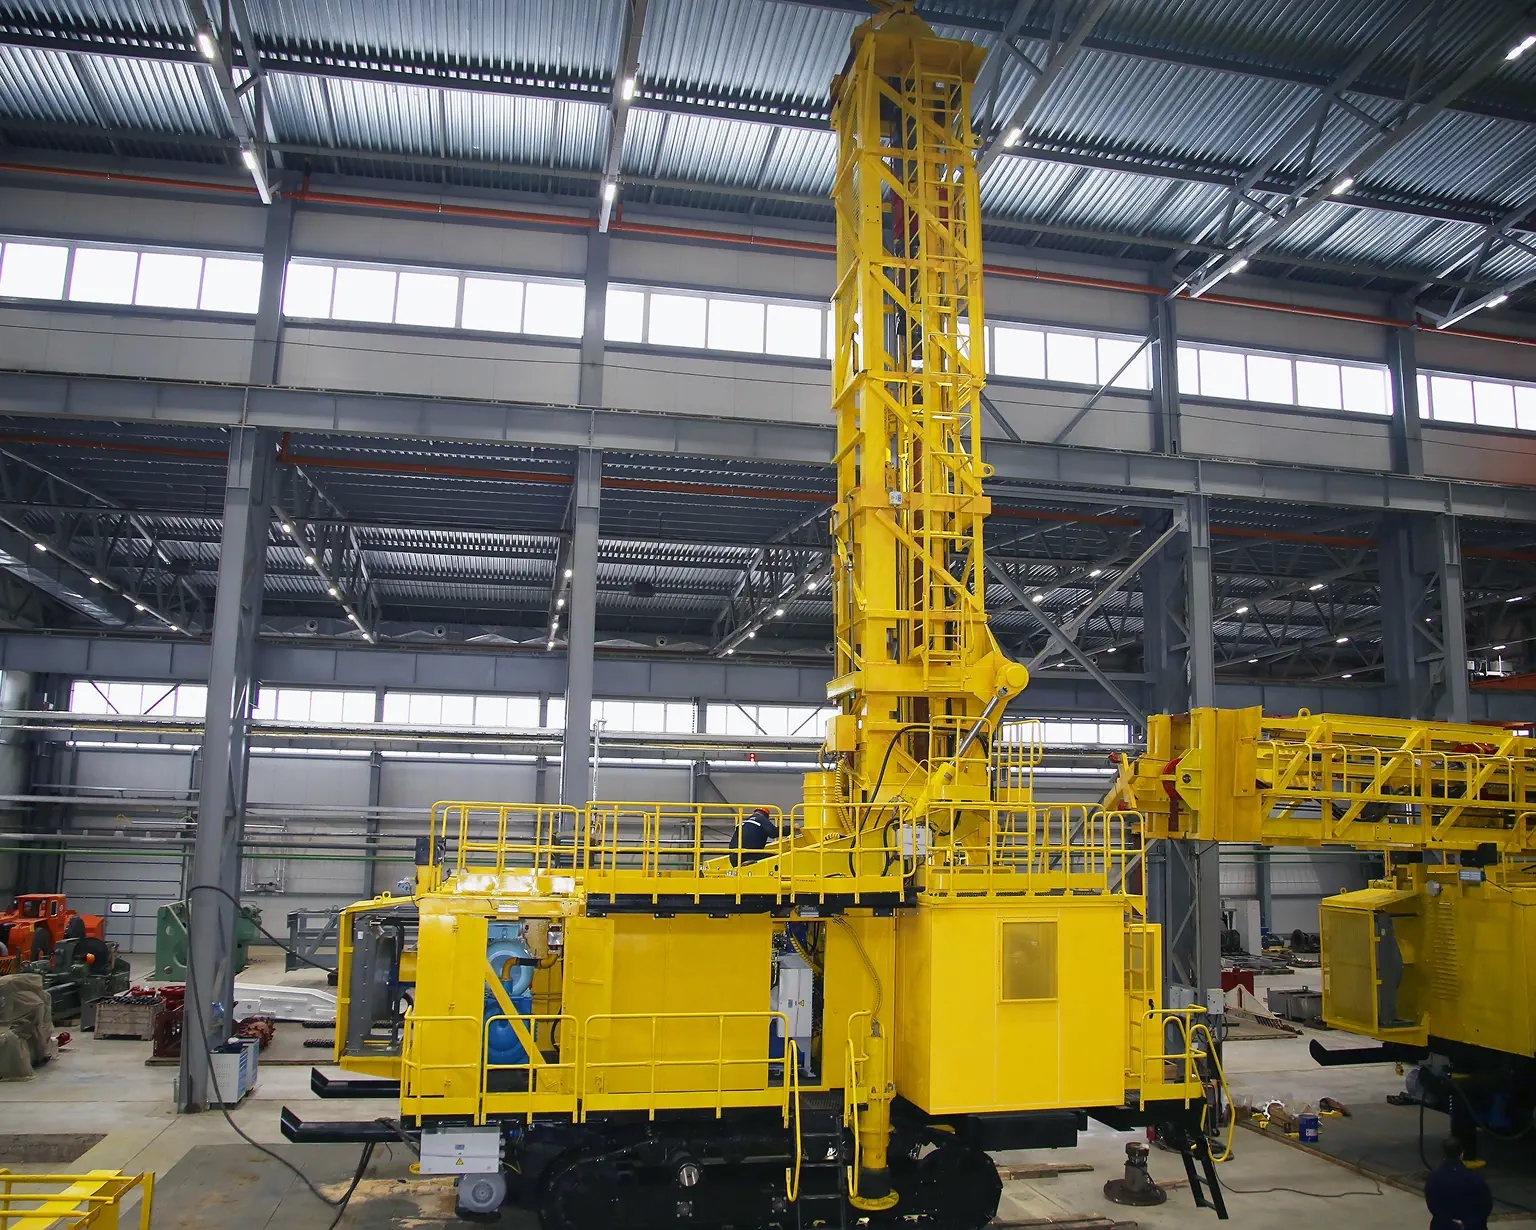
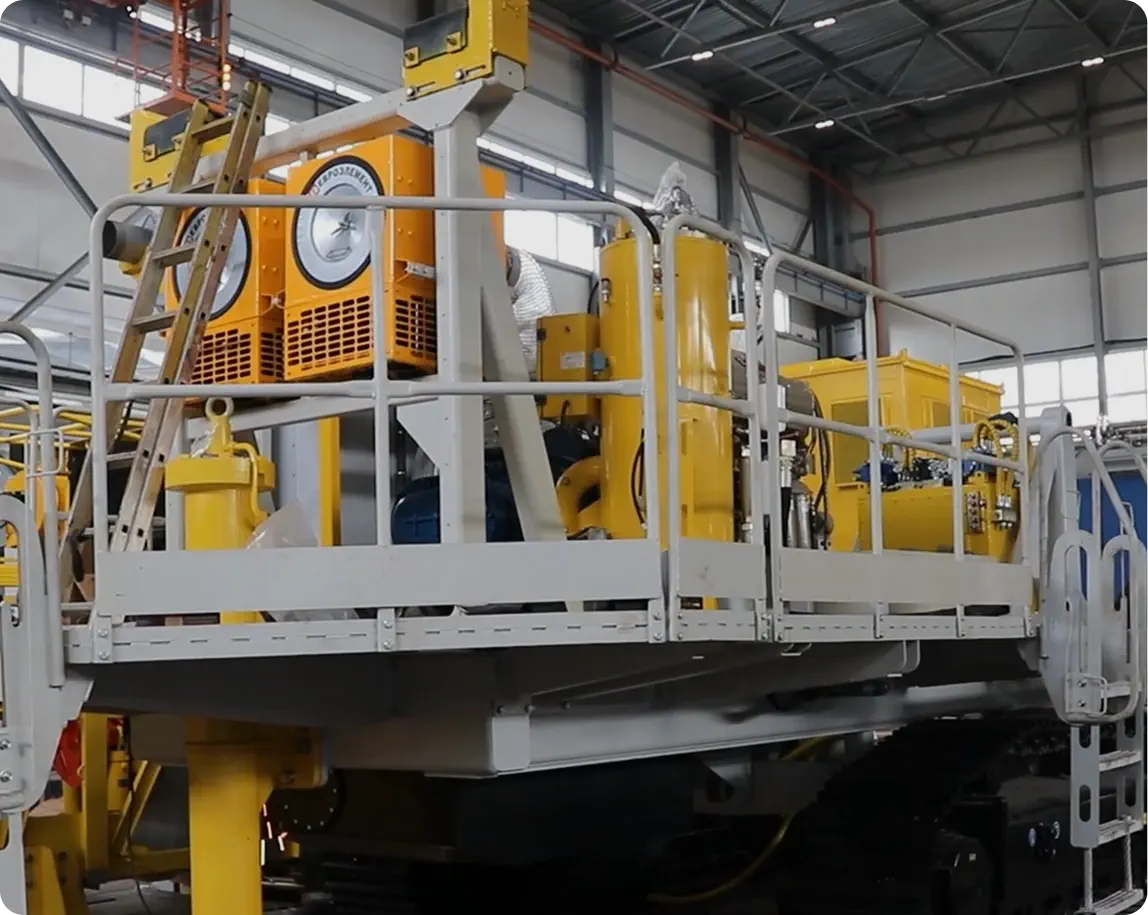
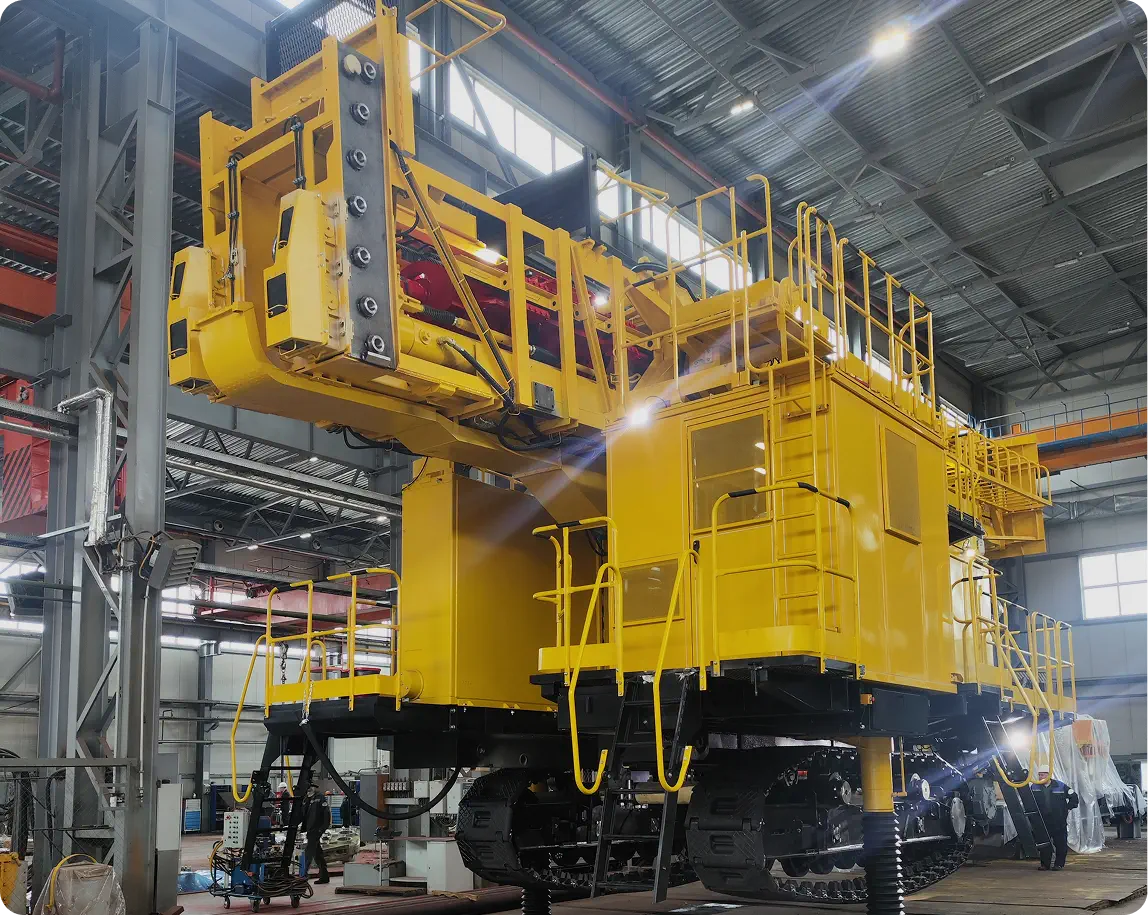
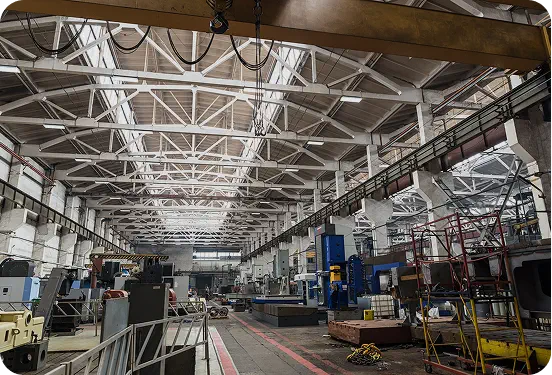
The structure and technical capabilities of the enterprise allow to carry out the complete production process, which is presented in the section "Products and services".
The plant park of the enterprise is represented by modern equipment of companies TOS WARNSDORF, FERMAT, DOOSAN, HYUNDAI WIA, HAAS, KLINGELNBERG HOFLER, SODICK, REMIX, KSM-SPB, NAKAL, VISTAN, VISAS and others. Requests already 7 days after the launch of the site’s quota Modern design and user-friendly interface Integration with analytics and CRM systems Possibility of refinements and extensions
Ensure high product quality and compliance with regulatory requirements
Successfully execute in-house orders
Fulfill orders of any complexity within the established deadlines for enterprises of other industries
Quickly get up to speed with new product types
Ability to process sheet and variety rolling:
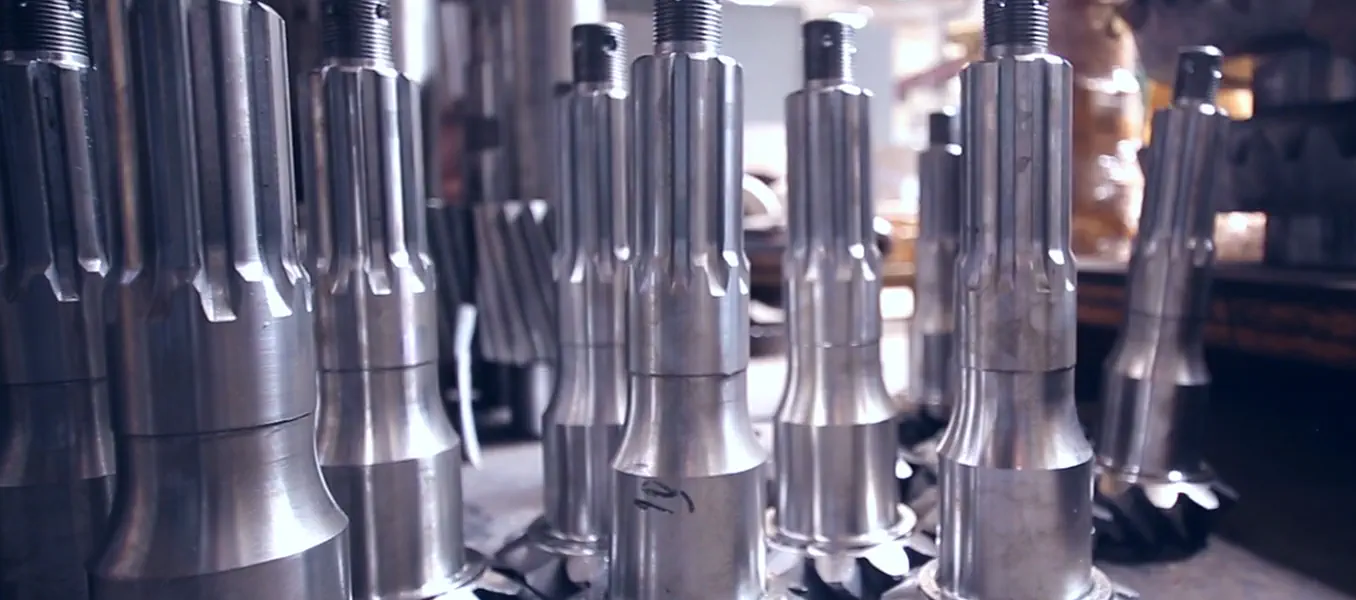
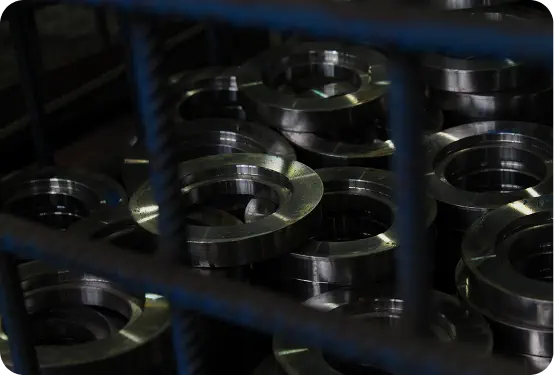
Manufacture on a steam-powered hammer with a mass of falling parts 2000 kg of GOST 7829-70 type forgings: disk with hole, disk without hole, sling with straps.
Outside diameter of the forging up to 900 mm, height up to 215 mm, mass up to 150 kg. Hot bulk stamping is carried out with a force of up to 1600 CE; the company manufactures the stamping fixture itself.
Press flex with CNC: length up to 3100 mm, sheet thickness up to 30 mm, force up to 5000 kN.
The rolling leaf is up to 3000 mm wide and 40 mm thick, with the possibility of conical production. Also carried out is the rolling of anchor anchors 26 mm long up to 1800 mm.
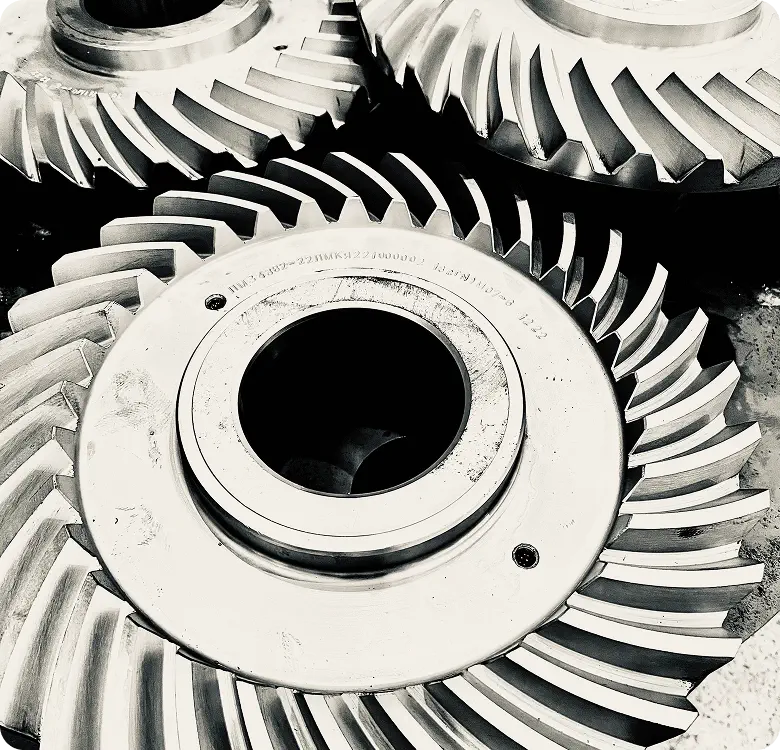
The company performs turning, boring, grinding, gear cutting, and milling operations on both conventional and CNC machine tools.
Machining capabilities accommodate large-scale components up to 11,000 mm in length, 4,000 mm in diameter, and 32 tonnes in weight. Operations include the machining of cylindrical, conical, and splined profiles, as well as gear components.
Wire-cut electrical discharge machining (EDM) is also utilized for parts with dimensions up to 950 × 700 mm and a weight of up to 1 tonne.
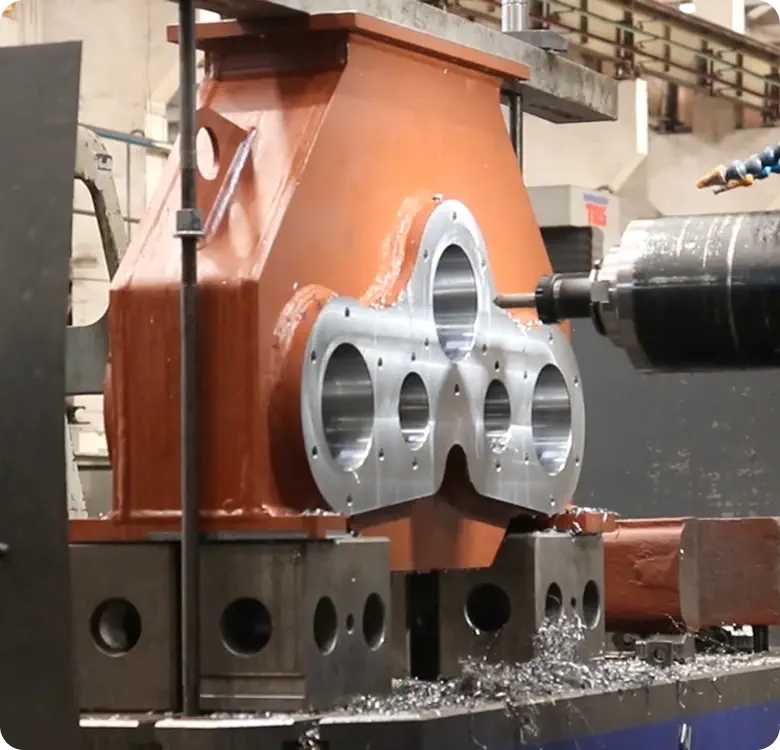
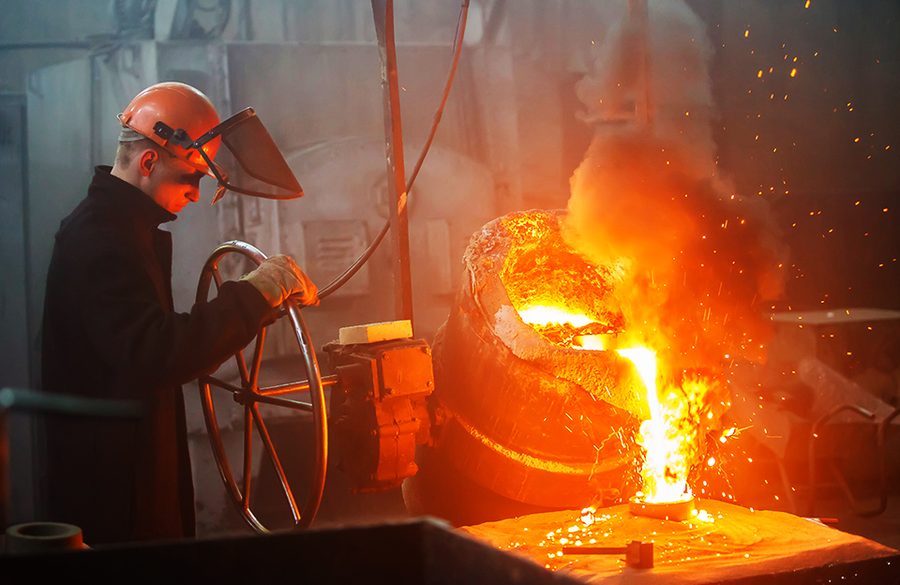
The heat treatment facility at RUP “RMZ Universal” is equipped with modern machinery capable of performing a wide range of thermal and thermochemical treatment operations on components and assemblies used in mechanical engineering.
The technologies employed ensure that products achieve the required mechanical properties, while also enhancing their wear resistance, strength, durability, and operational reliability.
The company provides heat treatment services both for its own production needs and for external organizations.
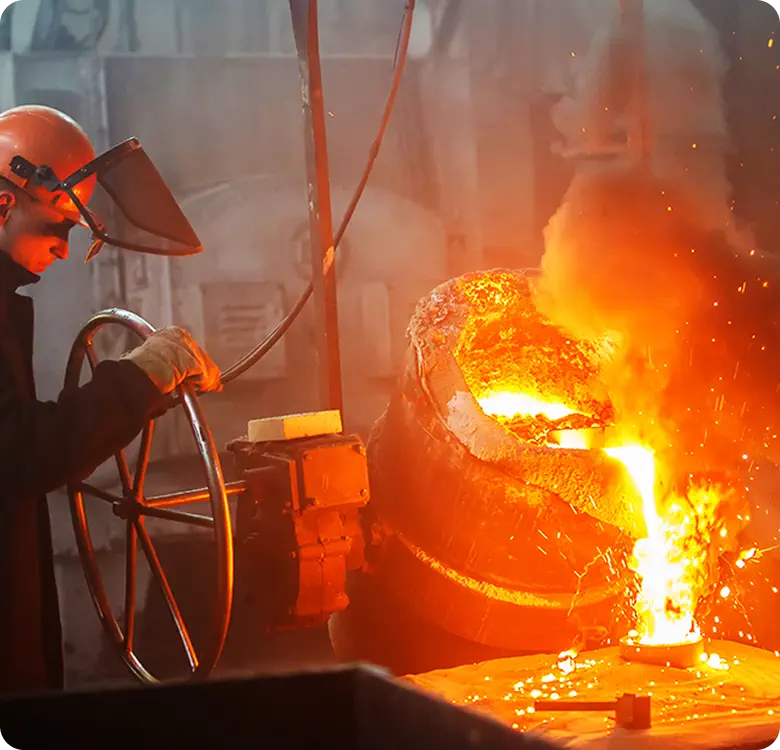
High-frequency induction hardening
Technical capabilities:
Shaft-type components:
Through-hardening
Technical capabilities:
Gas Carburizing
Technical capabilities:
Annealing, Normalizing, and High-Temperature Tempering
Processes performed:
Technical capabilities:
Heating in a Salt Bath
Technical capabilities:
The heat treatment department at RUP “RMZ Universal” possesses the production capacity to fulfill orders of varying complexity. We offer heat treatment services for machine-building components and assemblies, catering to enterprises within the Republic of Belarus as well as international partners.
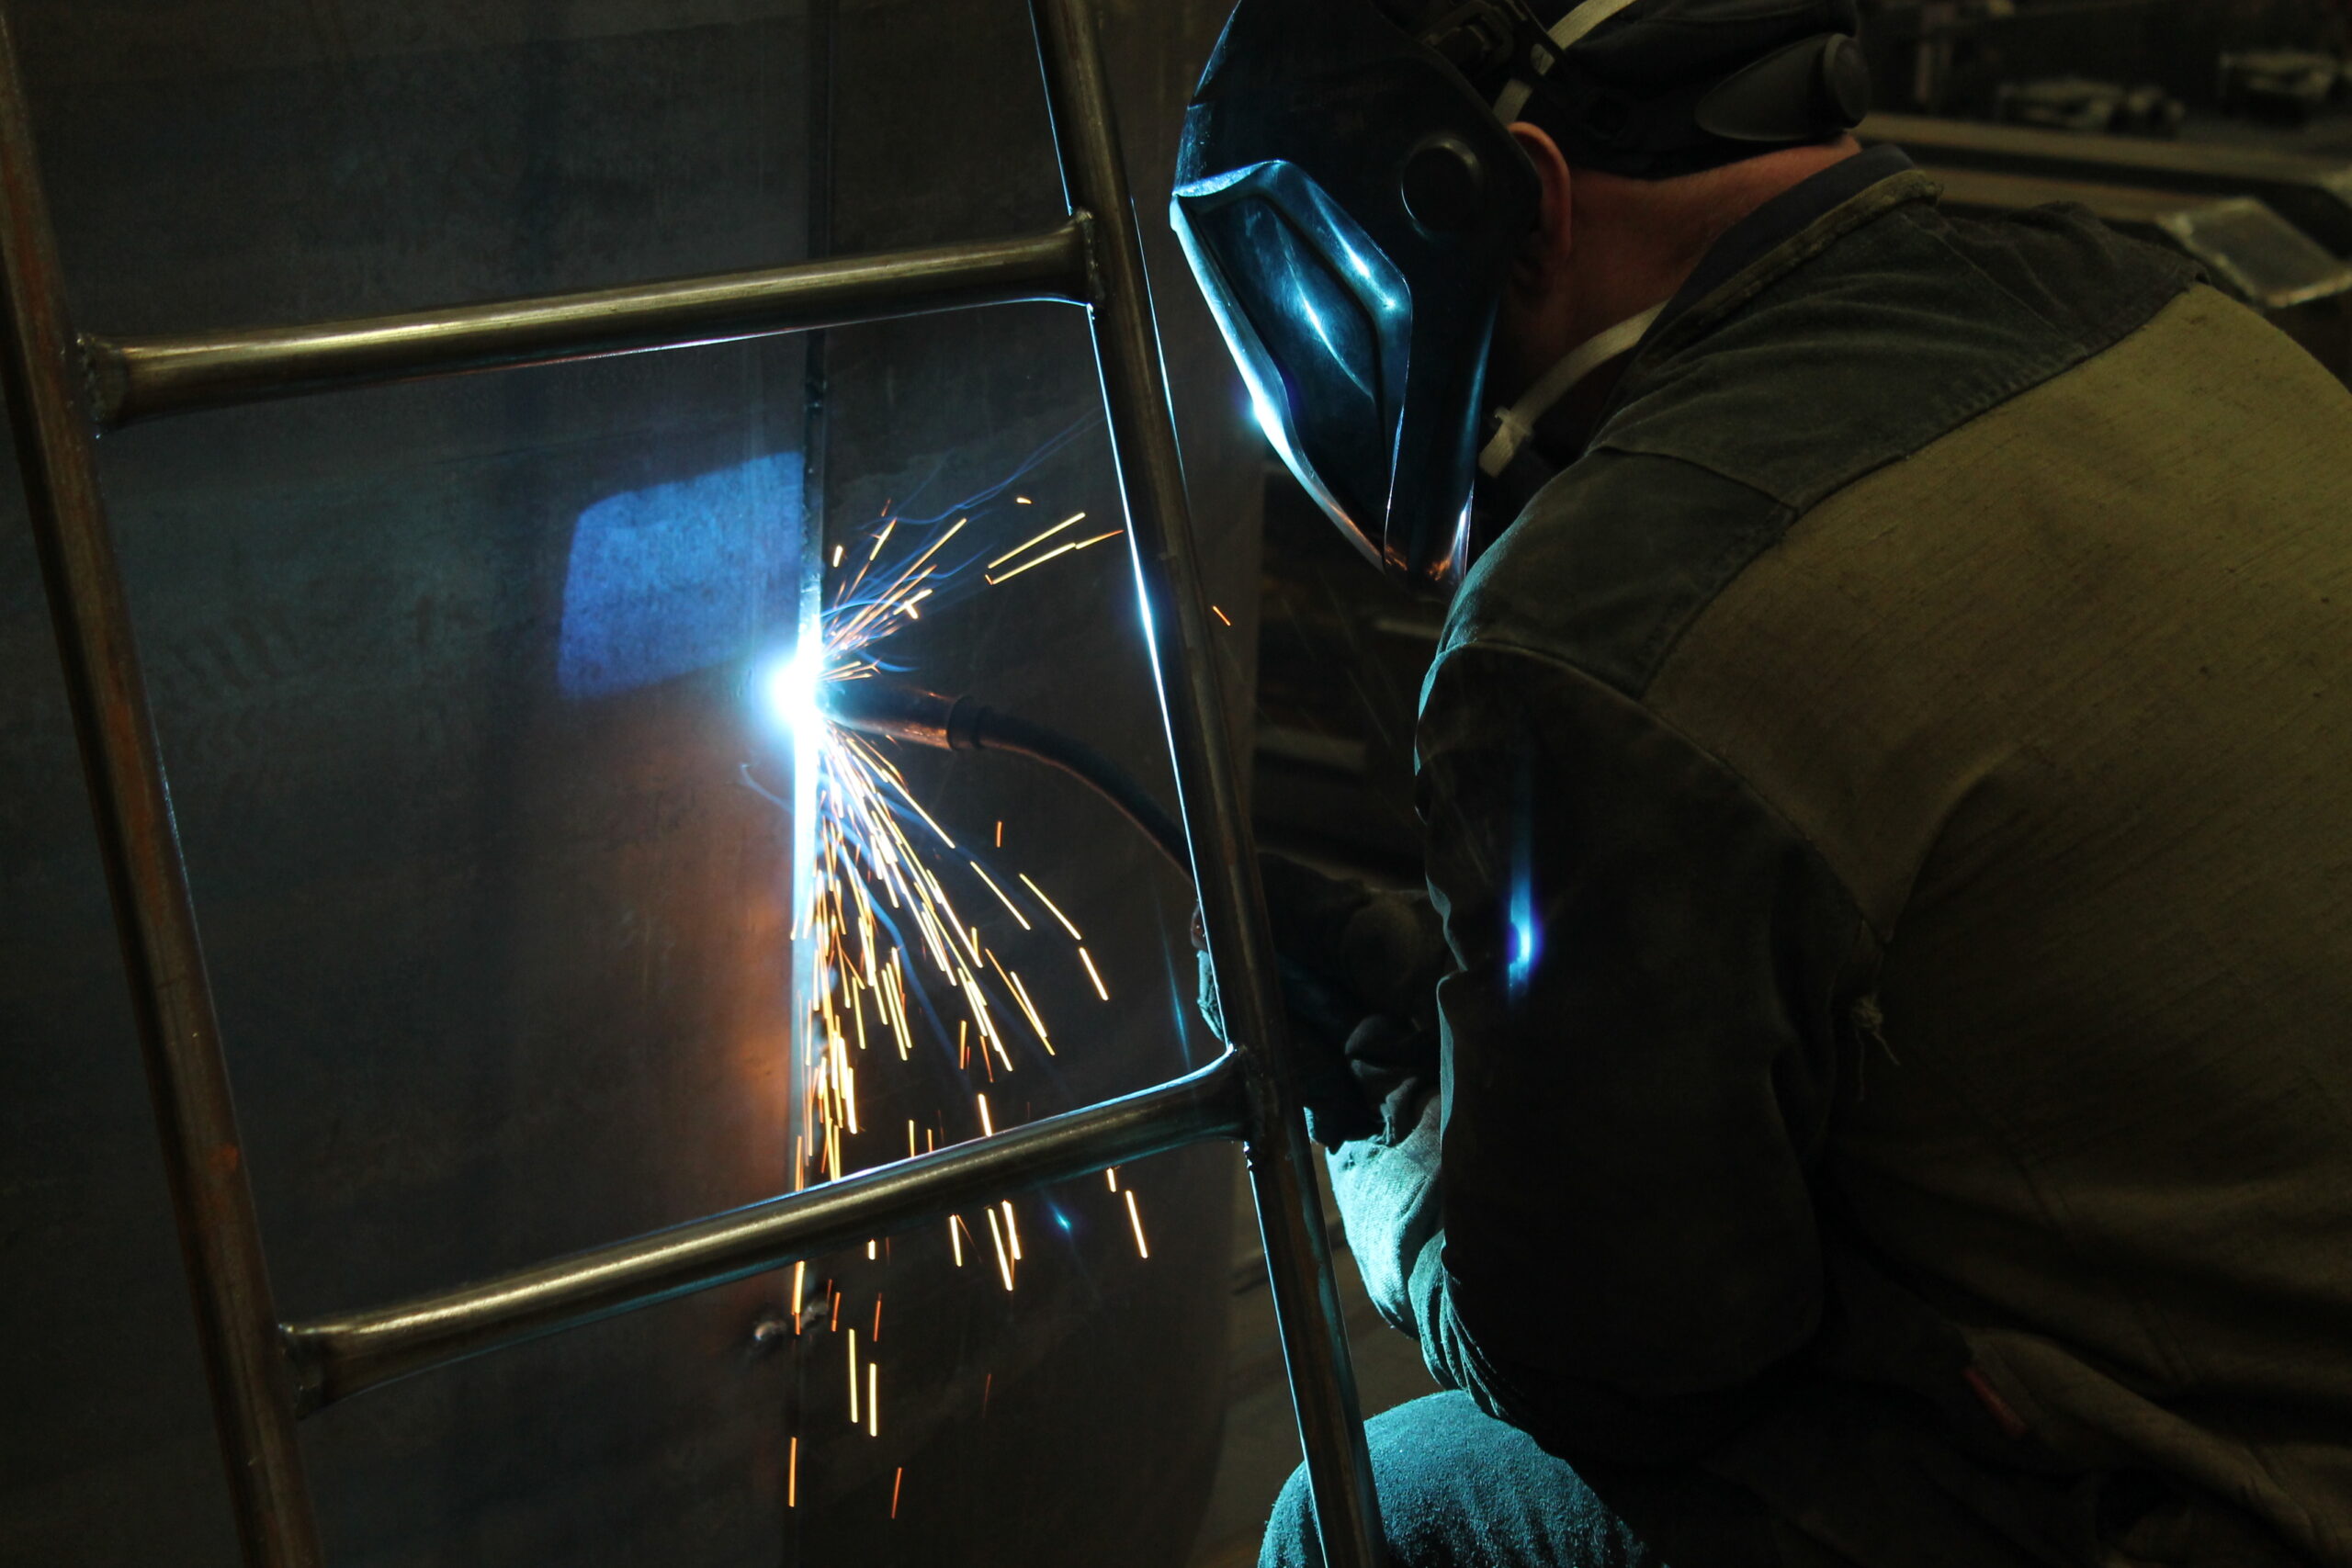
The facility possesses an extensive inventory of welding equipment, categorized by welding process:
A wide range of welded joints and metal/alloy surfacing operations are performed.
A wide range of welded joints and metal/alloy surfacing operations are performed.
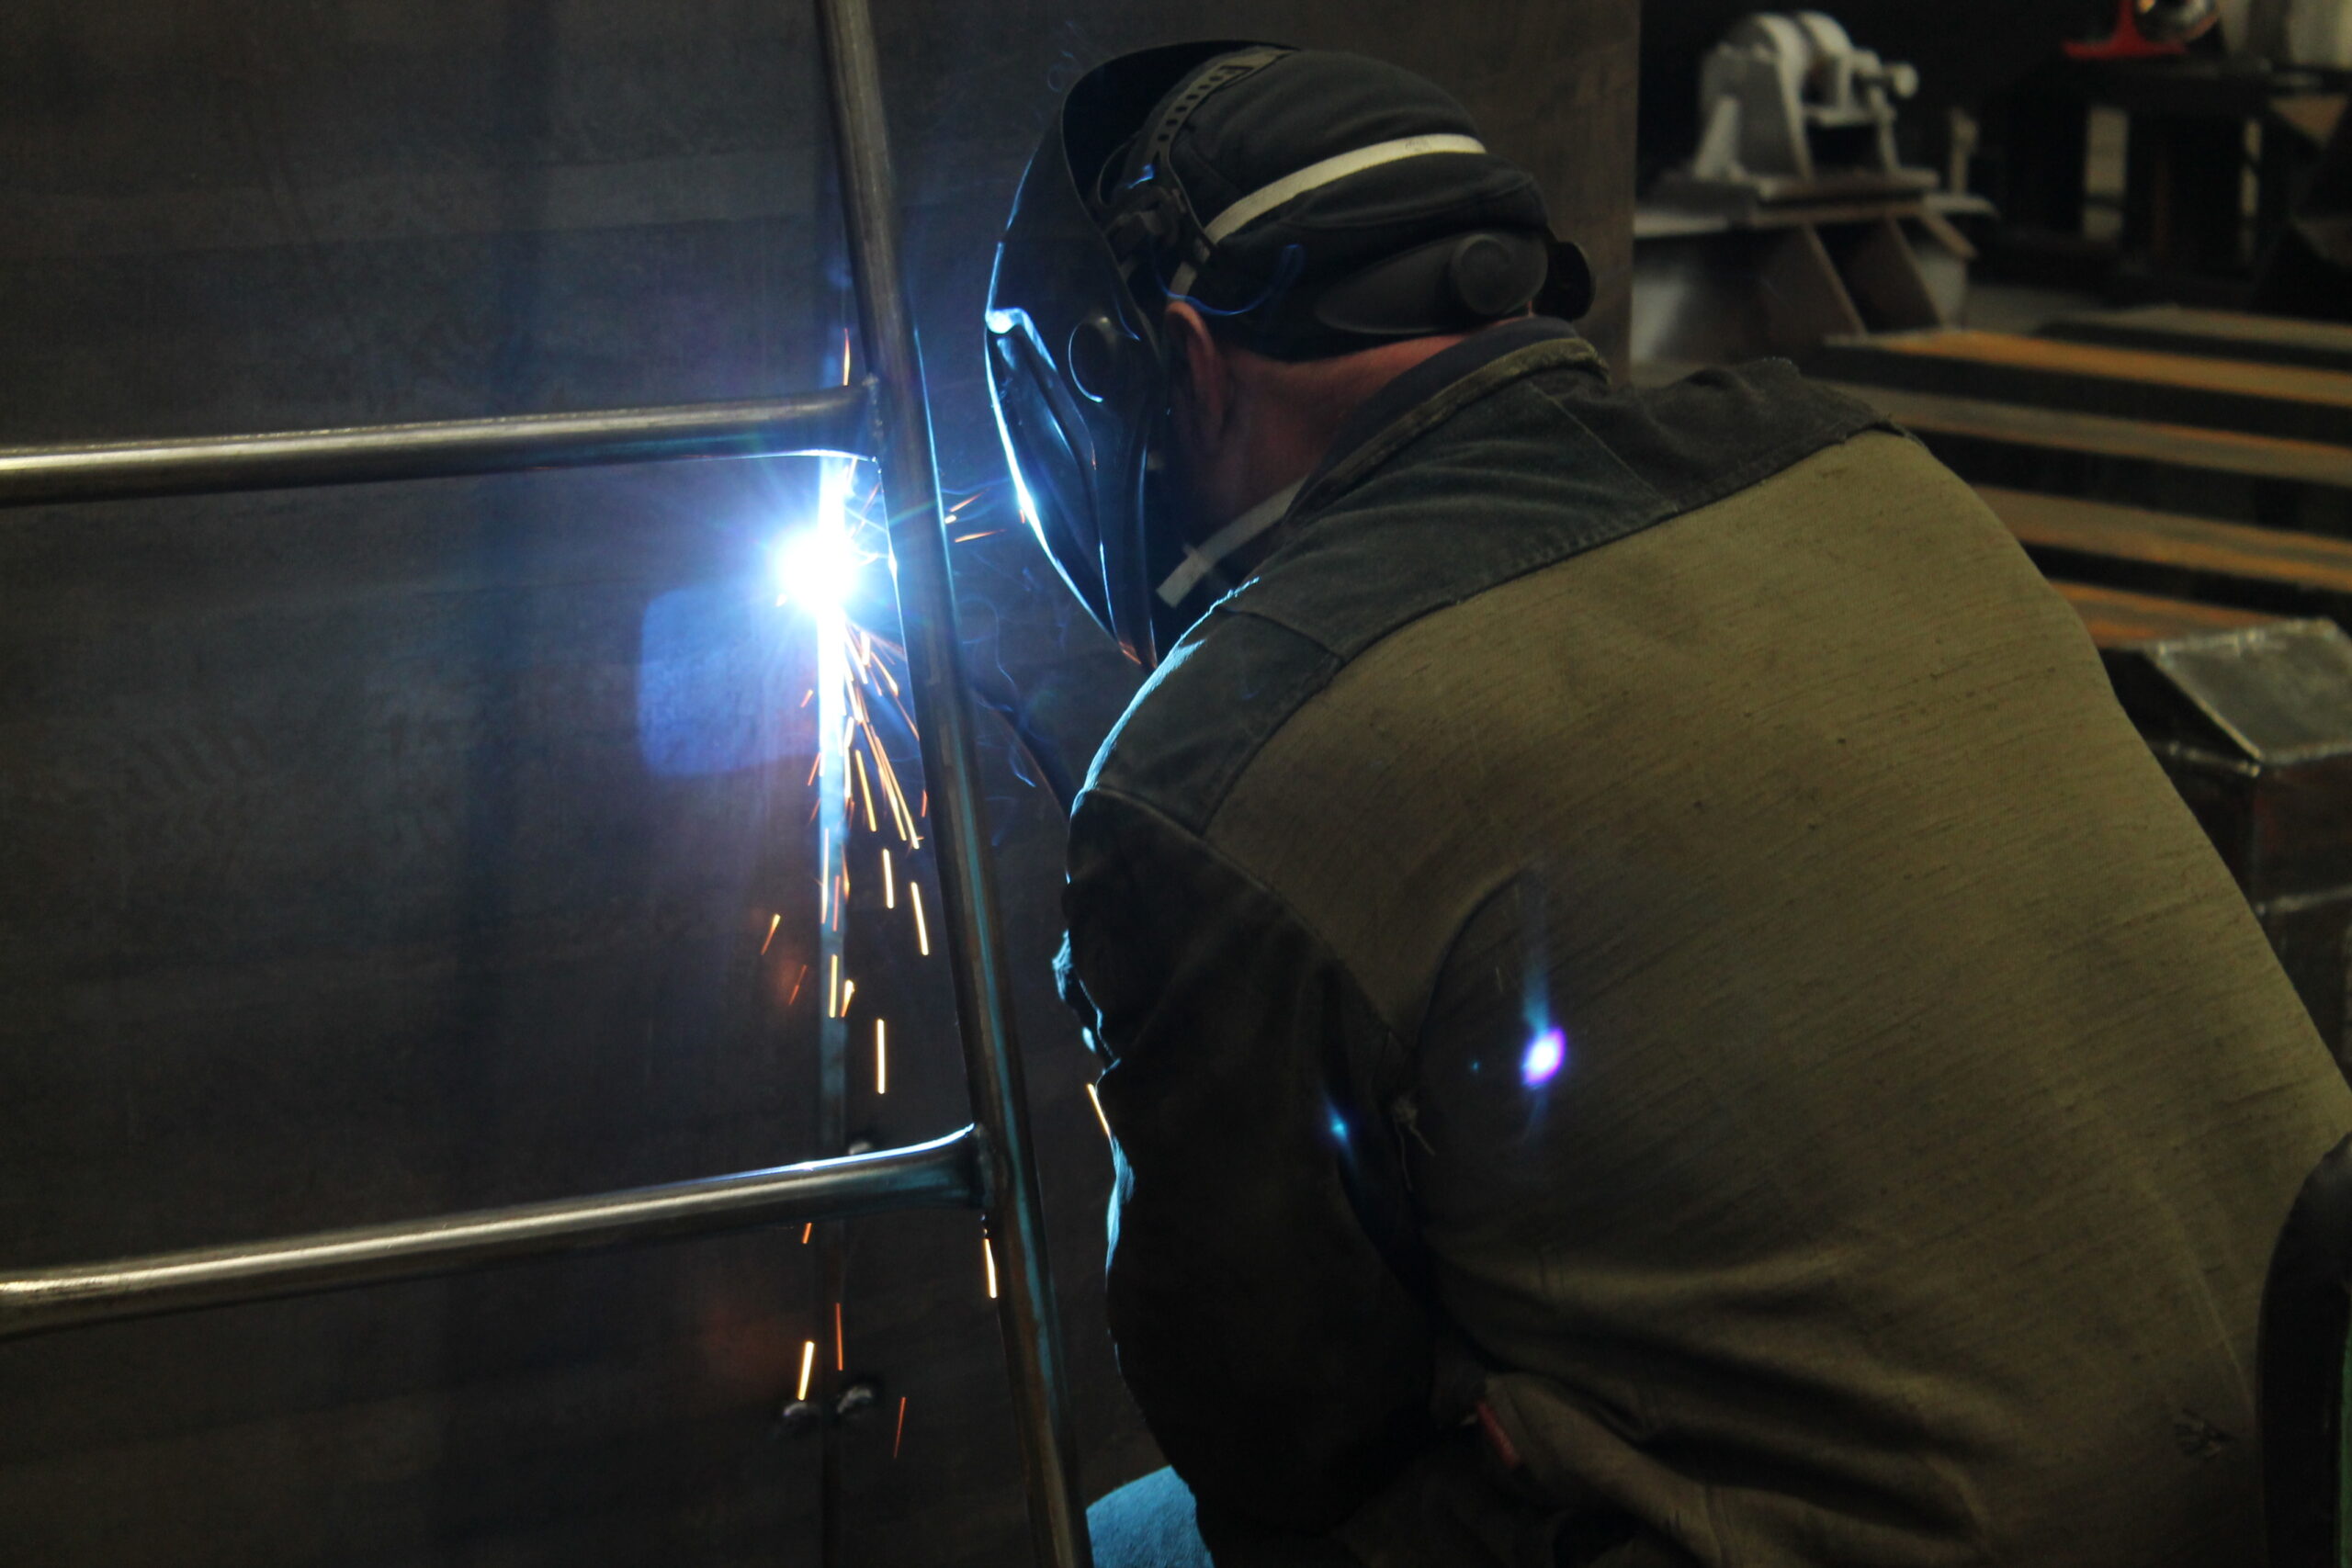
In our view, submerged arc welding is unique, as it allows for the welding of longitudinal and circumferential seams on cylindrical shells—without the need for edge preparation or a separate root pass—by using a flux backing.
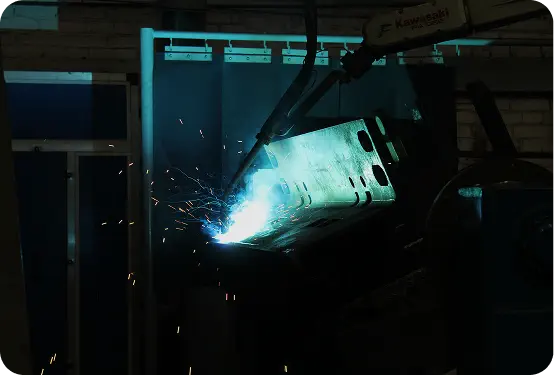
Another advanced method we employ is robotic welding, which performs welding in a shielding gas environment according to a pre-set program. This approach minimizes the need for operator intervention, thereby eliminating human error and ensuring a straight, uniform weld bead. The width and reinforcement of the weld comply with the GOST 14771-76 standard, featuring a smooth transition to the base metal.